CNC retrofits that put a sound machine back to work on a modern control
The record behind it
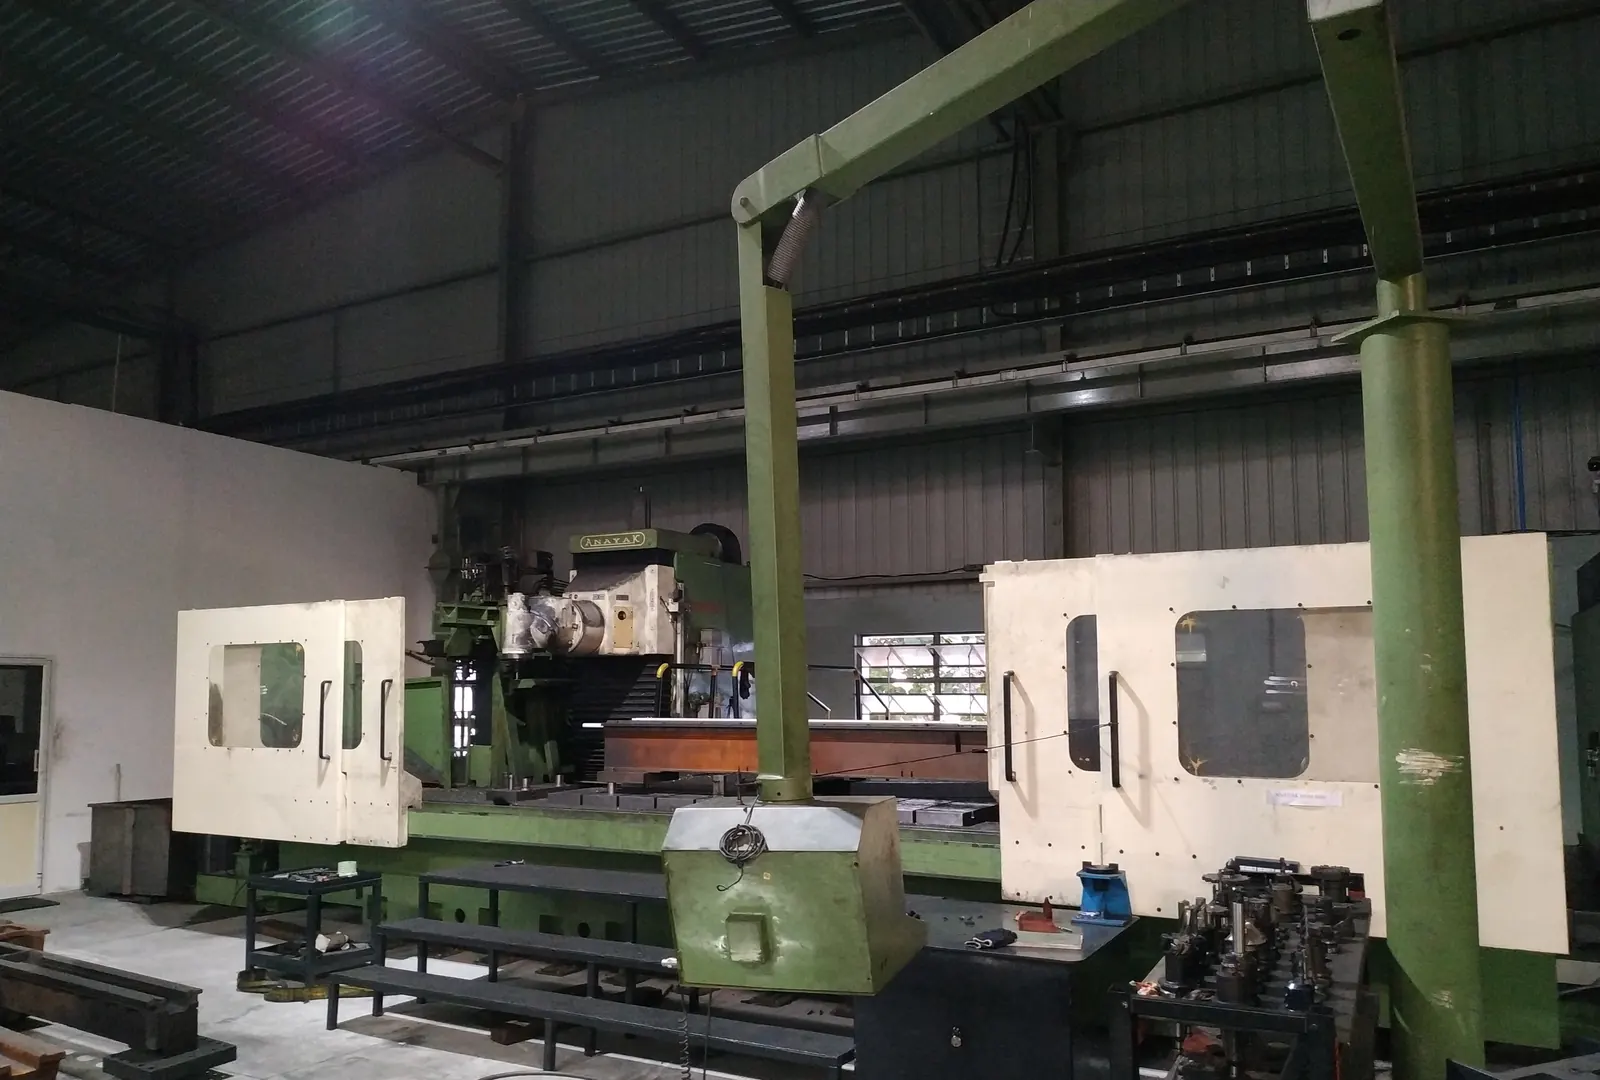
Between 2018 and 2022 our founder retrofitted more than 20 machines for machine shops around Coimbatore — VMCs, HMCs and turning centres from Anayak, Hartford and Haas — onto Fagor 8055i, Siemens 828D and Fanuc controls. That covered controller and servo selection, pneumatic and electrical panel design, PLC programming, commissioning, operator training, and the techno-commercial proposals and bills of quantity that went with them.
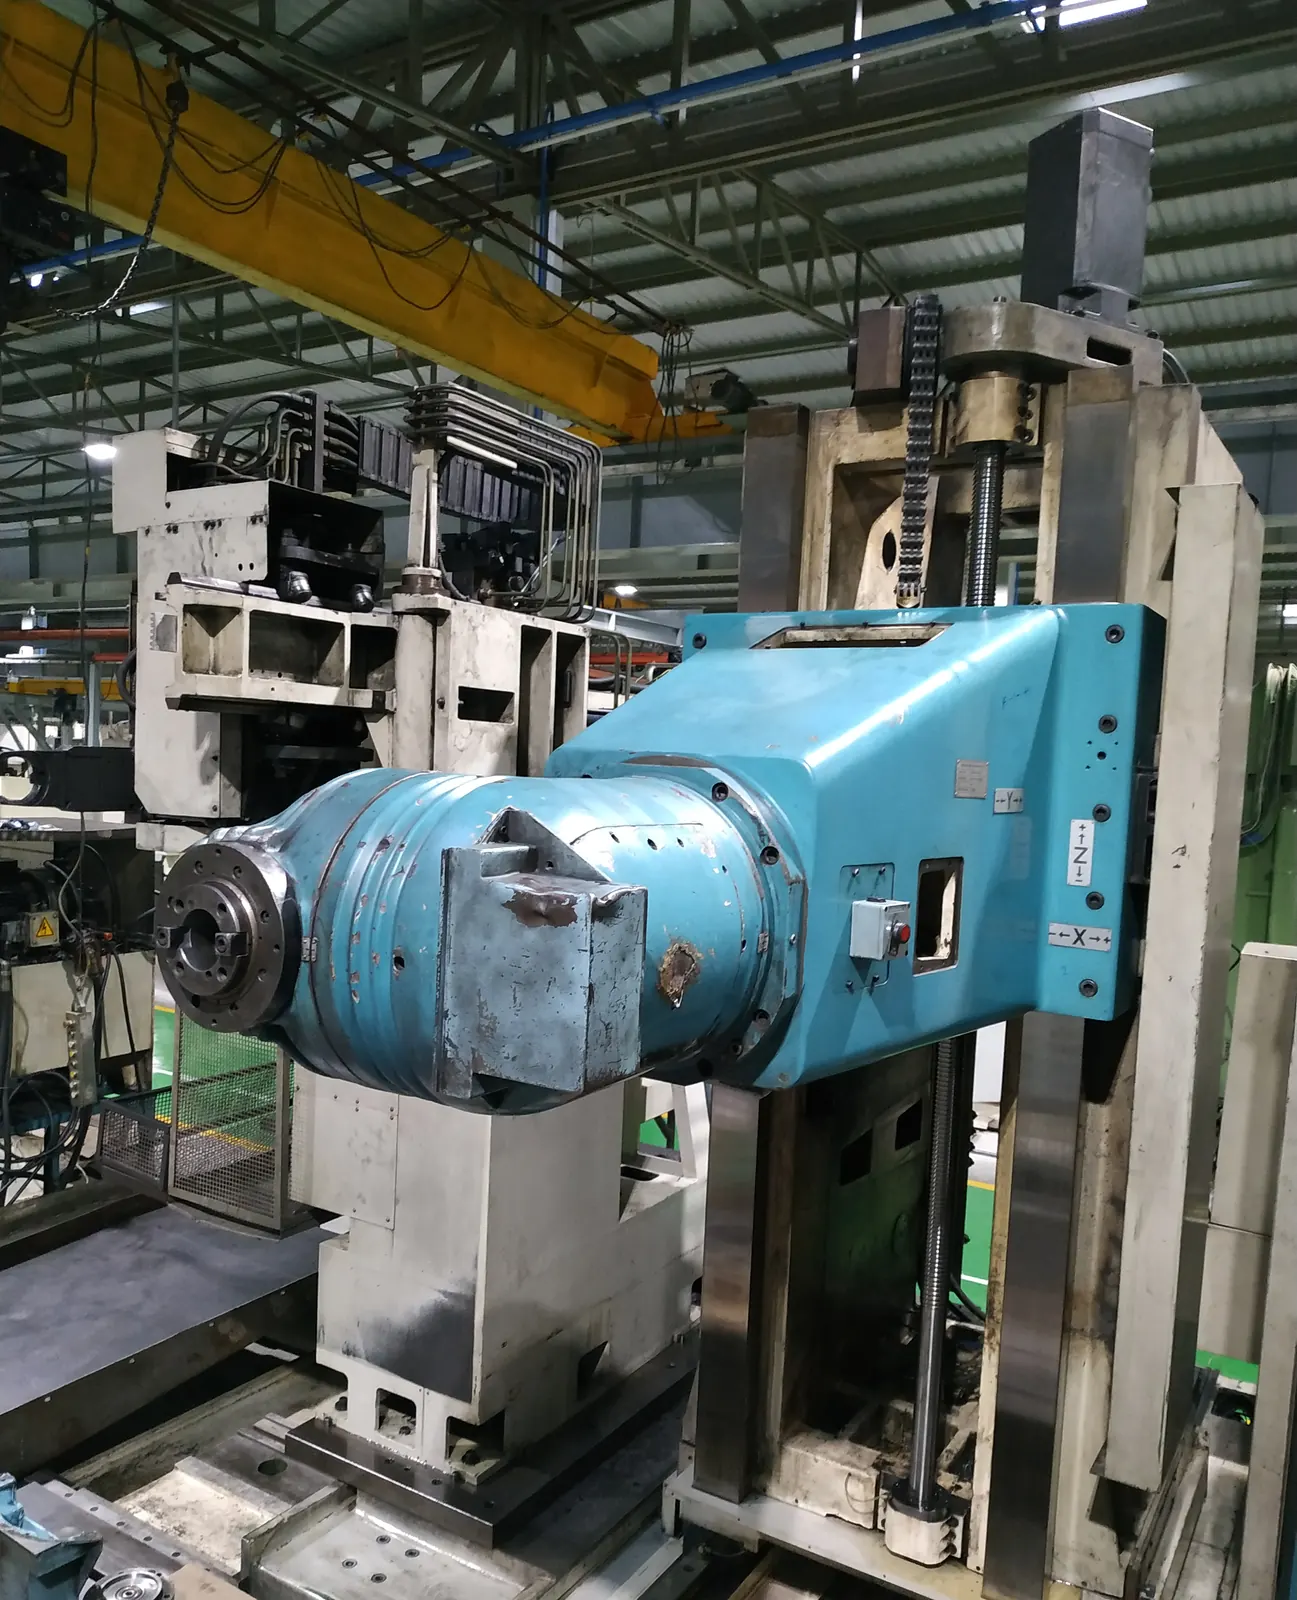
The video above is one of them: a large Anayak milling machine, retrofitted, changing its milling head automatically — a sequence that lives in the machine's PLC.
On the job
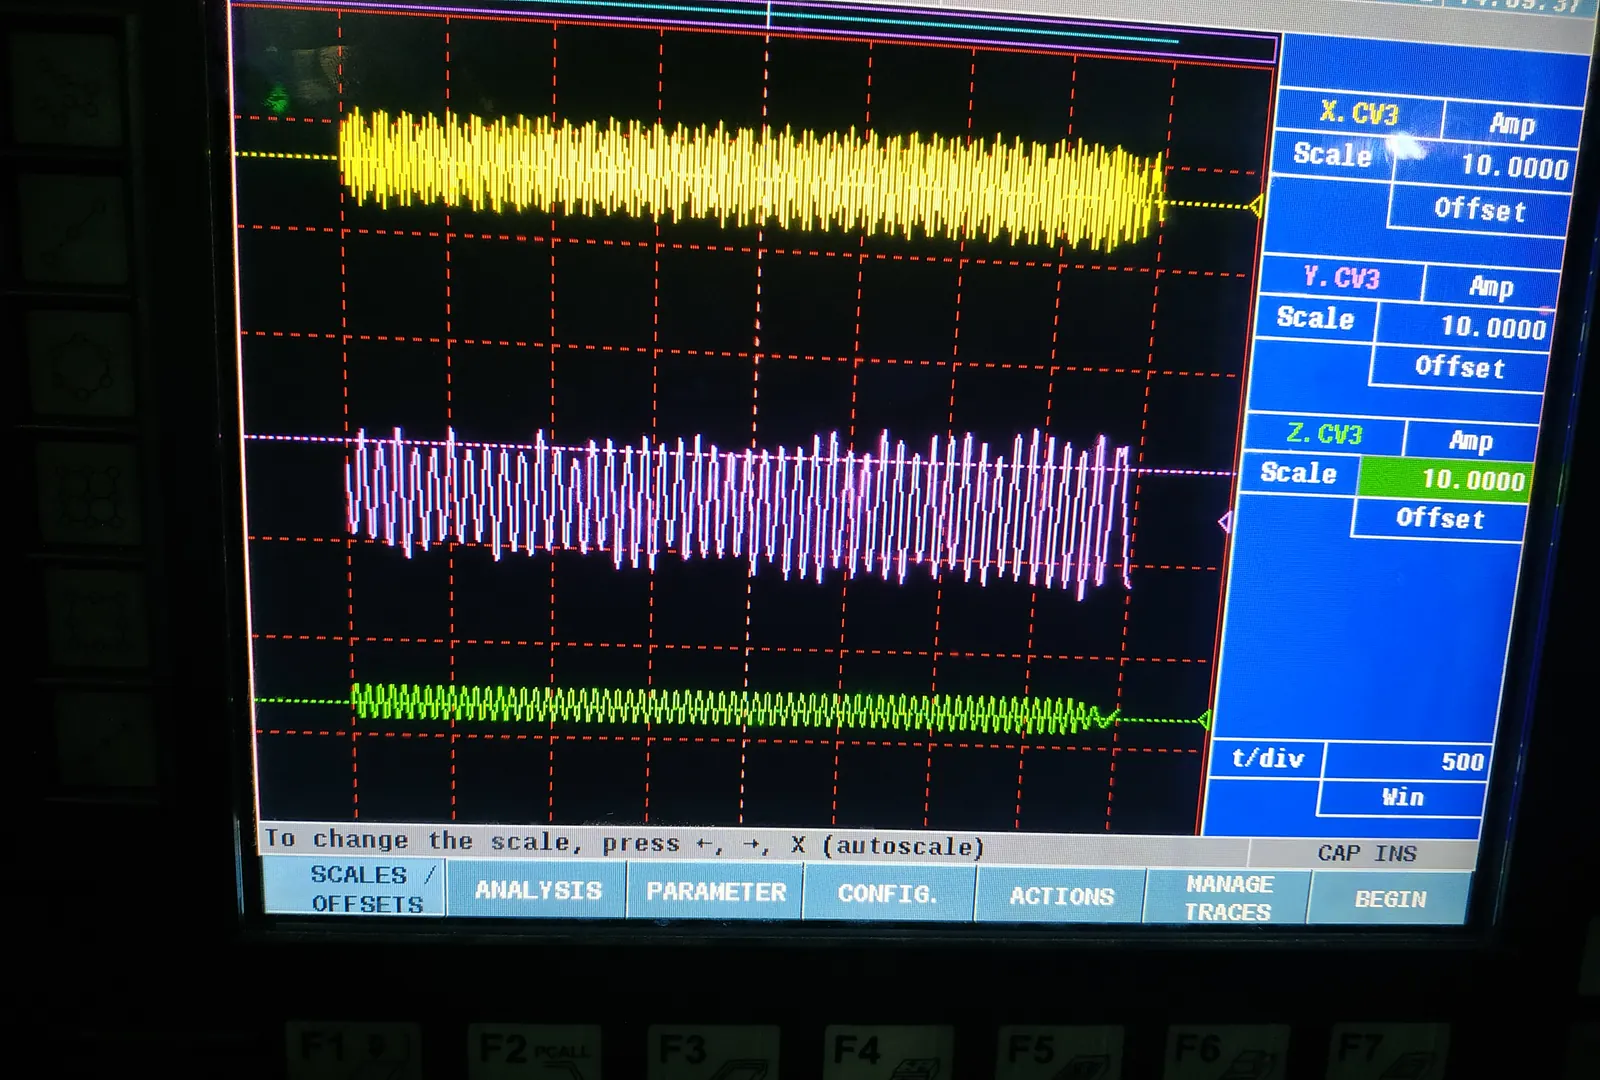
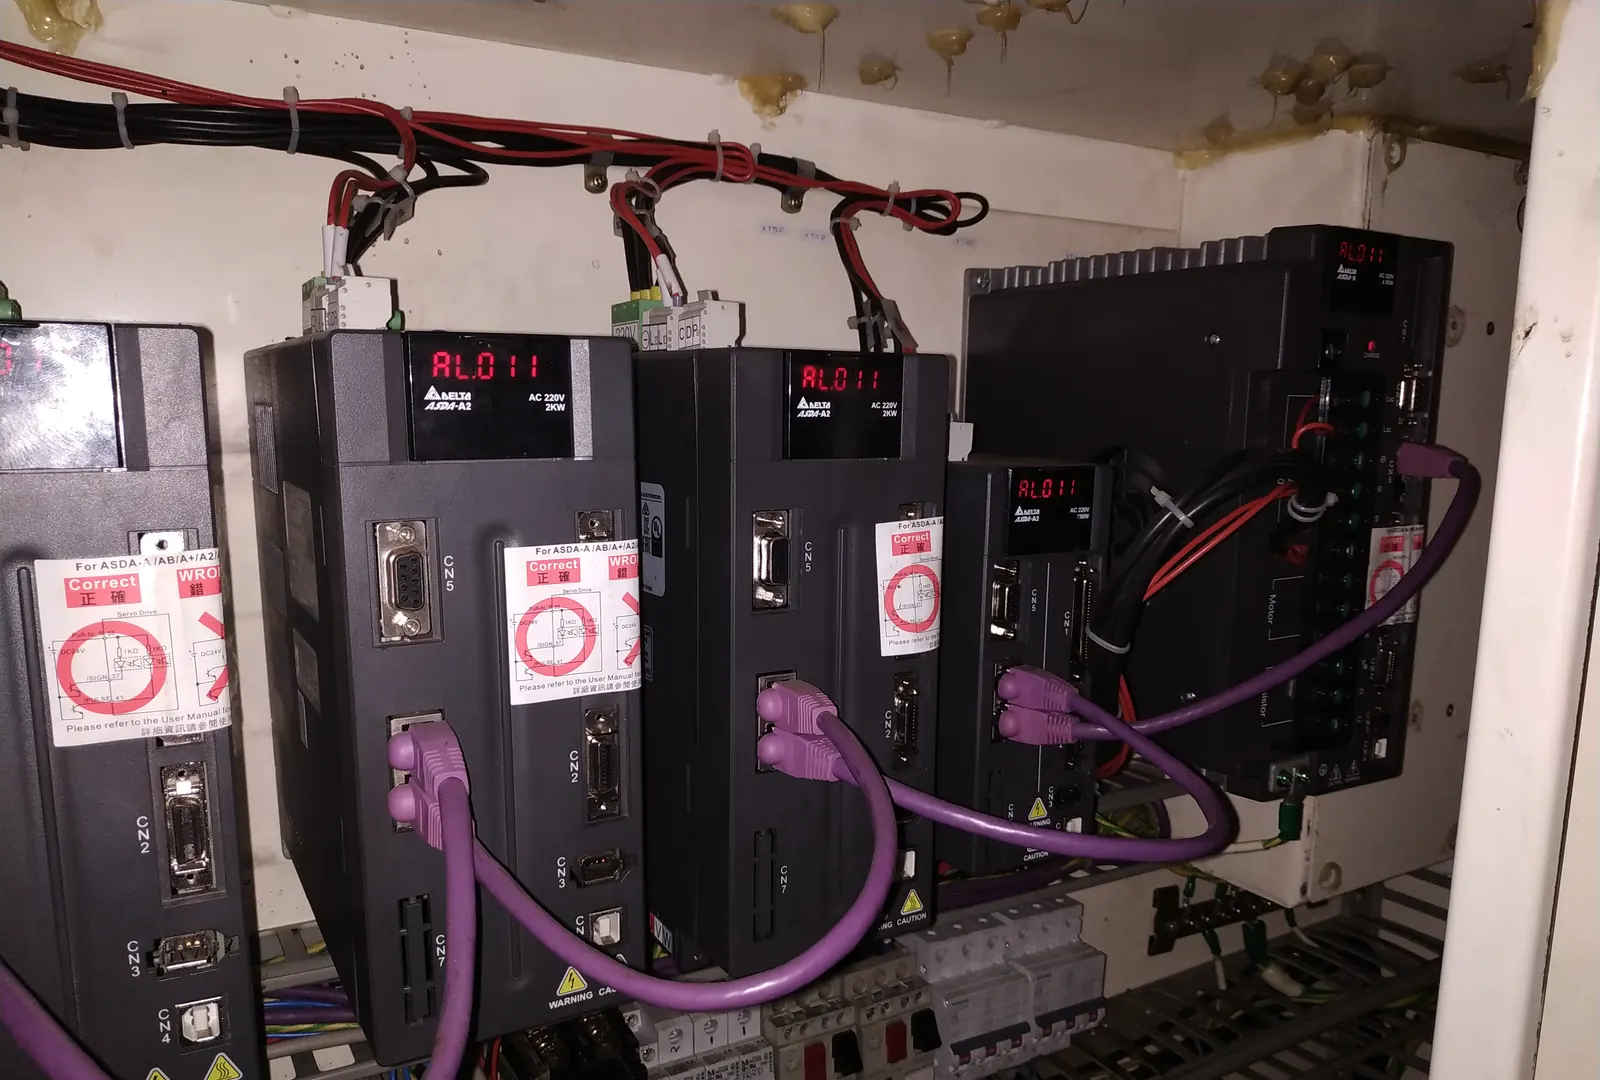
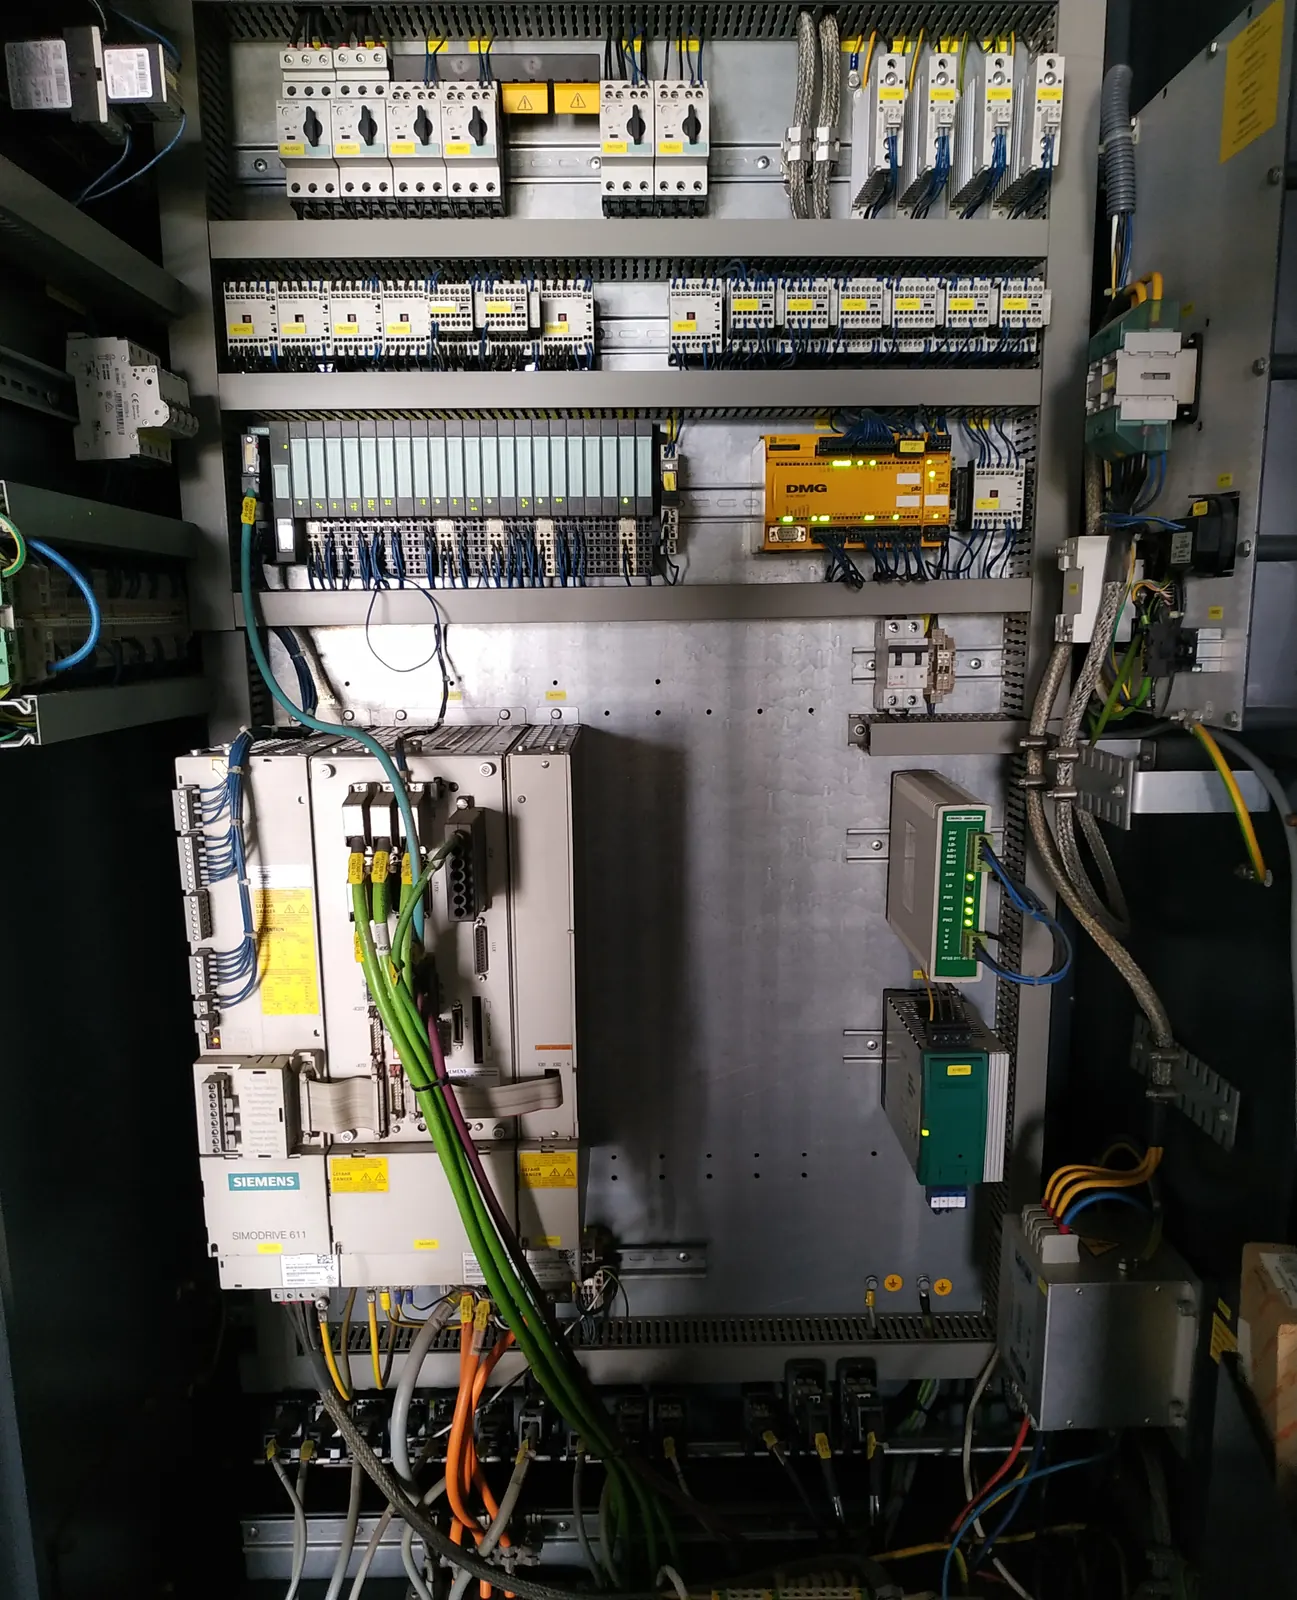
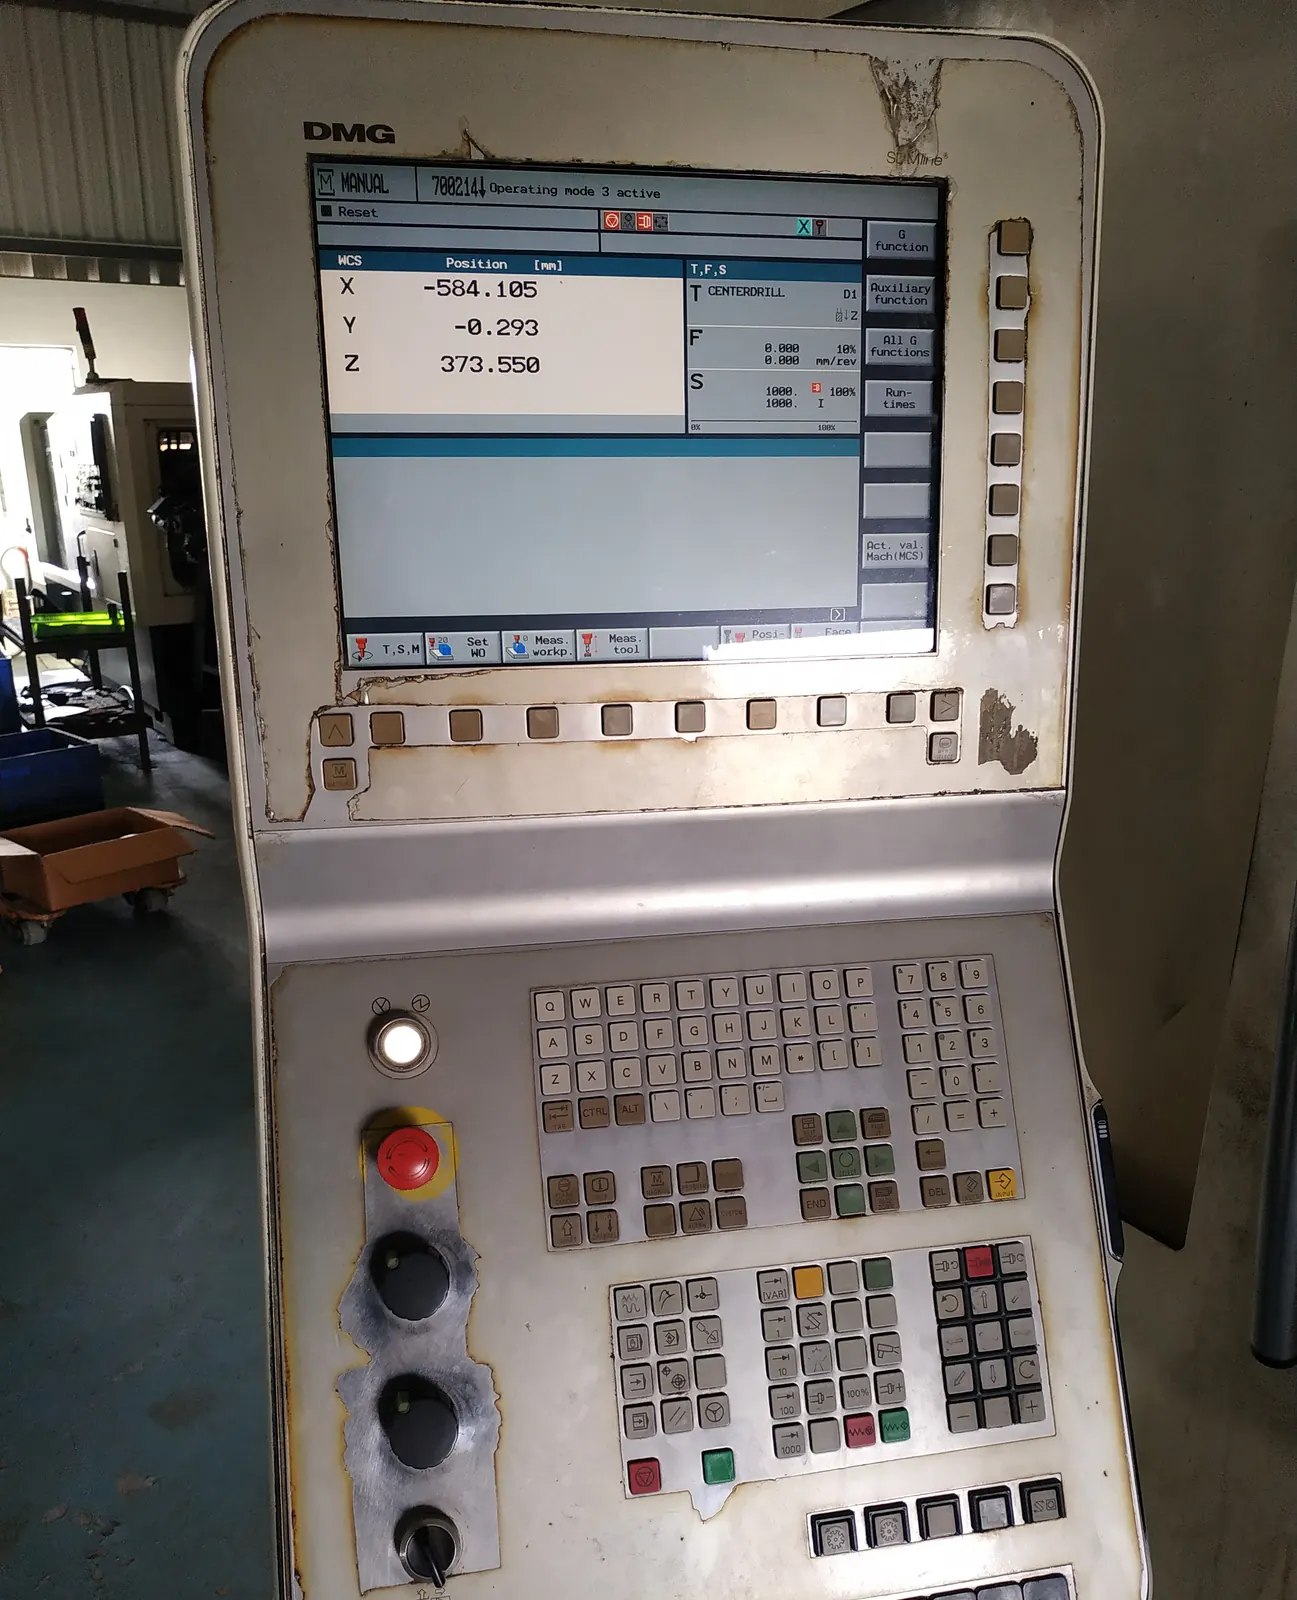
From retrofit jobs: the machine, the drives and the tuning.
What a retrofit covers
- Inspection of the mechanics first — a new control on worn iron is money wasted.
- Control, servo drive, motor and spindle drive selection to suit the machine and your shop.
- A new electrical panel, designed and drawn, with the old wiring removed rather than reused.
- PLC / PMC ladder for the machine's own functions: tool changer, head changer, lubrication, coolant, guarding.
- Axis tuning with the control's own oscilloscope, then backlash and pitch error compensation.
- Acceptance cutting, operator and maintenance training, and the drawings and parameter backups.
Once the machine is on a modern control, moving programs to it should not mean a pen drive. ElectronIx DNC sends, receives and drip-feeds programs to Fanuc controls over Ethernet or RS-232 from one PC.
Send the make, model, current control and a few photos of the machine and its panel. We will tell you whether it is worth retrofitting before anything else.
CNC retrofit questions
Retrofit or buy a new machine?
Retrofit when the iron is good — castings, slideways, ball screws and spindle in sound condition — and it is the control, drives or electrics that are failing or impossible to get spares for. A large or heavy machine is where a retrofit pays best, because the mechanical part is the expensive part to replace. If the mechanics are worn out, a new control will not save it, and we will say so after the inspection.
Which control should we choose?
Usually the one your operators and programmers already know, so programs and training carry over. Fanuc, Siemens 828D and Fagor 8055i all work well; the choice also depends on the axis count, the spindle and the spares support you can get locally.
How long is the machine down?
Most of the work — panel build, PLC and parameter preparation — is done before the old control comes out, so the machine is down only for removal, installation, wiring, tuning and acceptance cutting. The plan, with that downtime, is part of the quotation.
Can the existing servo motors be kept?
Sometimes. It depends on whether their encoders and ratings suit the new drives. Where they do, keeping them saves cost; where they do not, forcing them to work costs more in tuning and reliability than new motors would.
Will the retrofitted machine work with DNC?
Yes — a new control gives you Ethernet or a clean RS-232 port, and ElectronIx DNC can send, receive and drip-feed programs to it from the office PC.
Have a job that a machine should be doing?
Send the part and the target output. You get a concept, a sequence and a budget range back — free, and with no obligation to build it with us.